Solutions

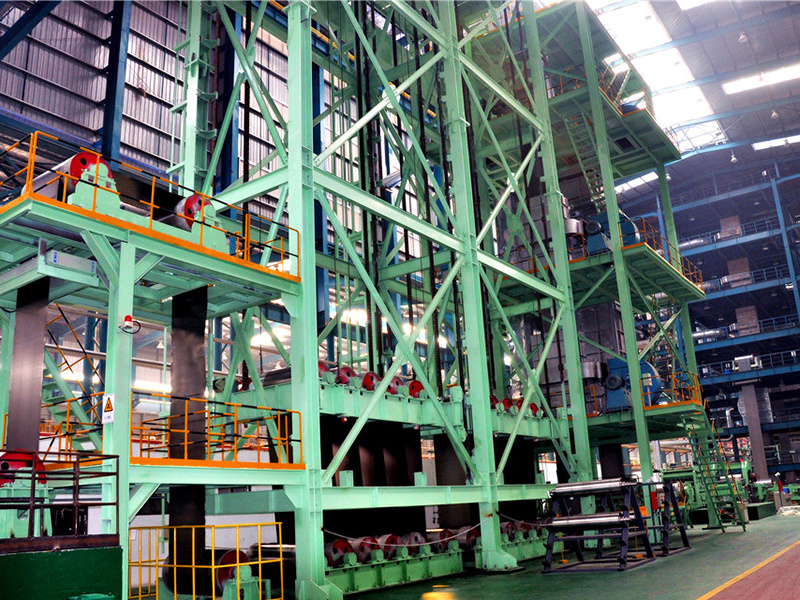
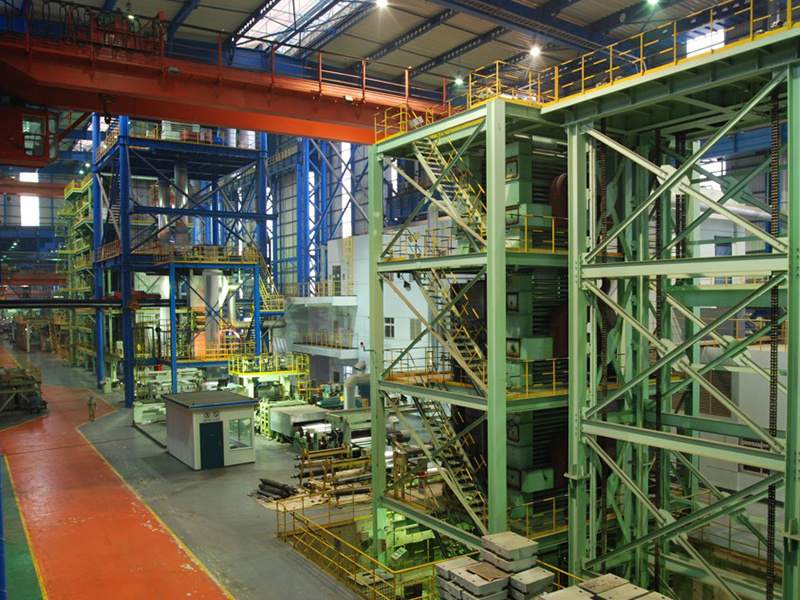
Continuous Pickling Line (CPL) for Carbon Steel
Category: Solution
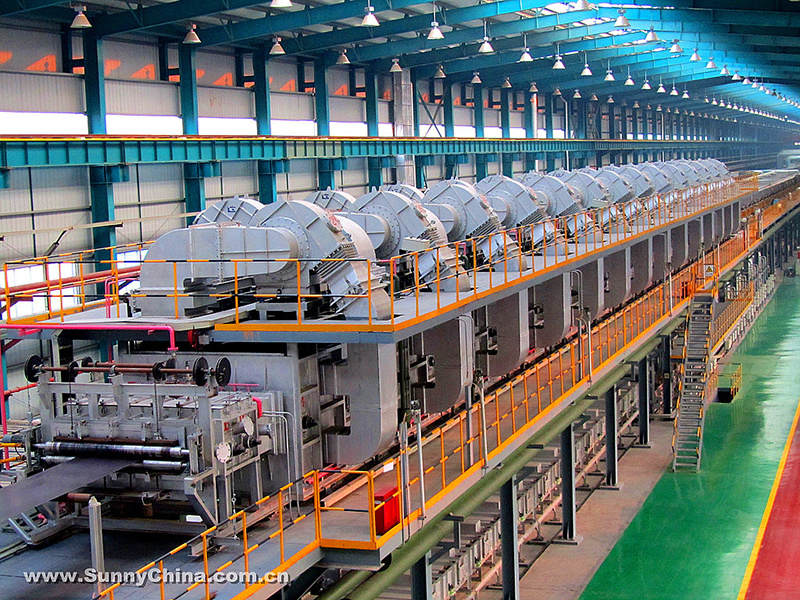
Using a continuous hydrochloric acid pickling process, the iron oxide layer on the surface of the hot-rolled strip is removed, and the irregular edges of the strip are cut off, providing qualified hot-rolled strip raw materials for the next process. The pickled strip has a pure iron surface and can be cold-rolled or hot-dip galvanized.
Details
This line uses a continuous hydrochloric acid pickling process to remove the iron oxide layer from the surface of hot-rolled strip steel and trim irregular edges, providing qualified hot-rolled steel for subsequent processes. The pickled steel has a pure iron surface and can be used for cold rolling or hot-dip galvanizing processes.
Features
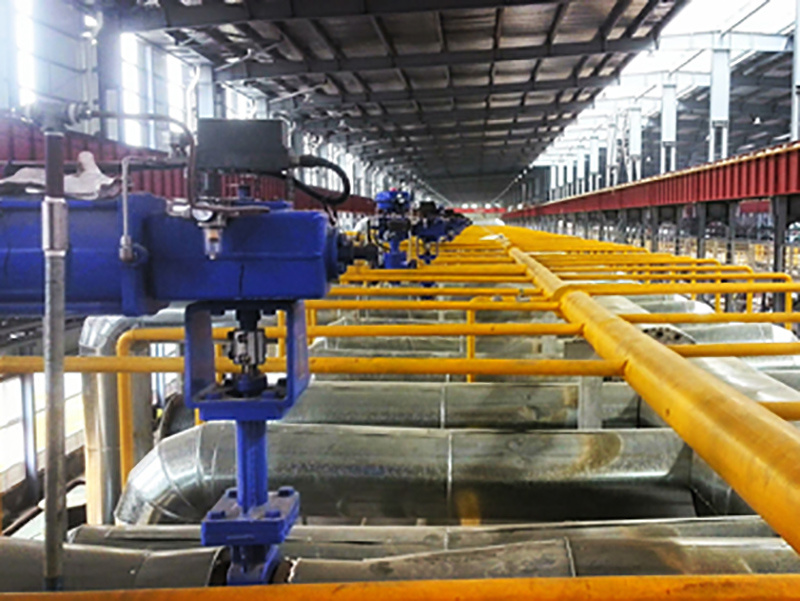
This continuous pickling line features an automatic argon arc welder and a descaling and straightening machine at the inlet. The process section uses a multi-stage shallow tank turbulent flow pickling process and a multi-stage water rinsing process. The outlet section includes a rotary shear and an electrostatic oiling machine.
Annual Production Capacity: 800,000-1,200,000 t/a
Raw Material: Hot-rolled carbon steel coils
Steel Grades: CQ, DQ, DDQ, IF, HSLA, W440-W1300 silicon steel
Raw Material Specifications: 1.5-6.0 mm x Width: 650-1650 mm
Coil Diameter: I.D. Φ760/Φ610 mm O.D. Max Φ2150 mm Maximum Coil Weight: 30 t
Hot-rolled Coil Entry Temperature: Max 670°C (IF < 720°C)
Process Speed: Max 150 mpm
Pickling Time: 25-30 sec
Uses SIEMENS or ABB electrical control system
Production Process Flow

Coil Loading -> Coil Unwinding -> Head Cutting -> Welding -> Inlet Loop -> Descaling and Straightening -> Pickling -> Water Rinsing -> Drying -> Outlet Loop -> Edge Trimming -> Oiling -> Slitting -> Coil Winding -> Coil Unloading -> Packaging
Related Solutions


SUNNY Technologies Incorporation Limited
WeChat Channel
Corporate Webslte
Contact us
Tel:
0086-156 7177 7755 / 0086-027-5971 5081(Marketing)
0086-027-5971 5061-8702(Purchasing)
0086-027-5971 5061-8522(HR)
0086-027-5971 5061(General)
Fax:
0086-027-59715060
Email:
Address:
#101,Gaoxin 6 Road,East Lake Hi-Tech Development Zone,Wuhan,P.R.China
#72, Xialu Avenue, Xialu District, Huangshi, P.R. China
COPYRIGHT © 2025 SUNNY Technologies Incorporation Limited. All rights reserved. POWER BY: 300.CN · [ Privacy Policy ]
 Wechat